Wear note
Aperture honesty beats hope
Screen media that lies about aperture sells product that customers reject.
By Ms Lerato Dlamini, Wear notes lead
Ms Lerato Dlamini leads wear notes at Crusher Consumables, giving plant leads practical advice on tackling tough, abrasive feeds that hammer crusher parts.
AuthorWhy this matters on the plant
In my years in the wear-parts game, I have seen more headache caused by dodgy screen apertures than almost any other issue on a plant. When aperture size on your screen media does not match what is marked, rejected loads and lost trust are not far behind.
Why accurate apertures matter
Aperture size is not just a number on the side of a panel. It is the make-or-break detail that determines what goes onto your product stockpiles and what ends up as reject. If you fit 10 mm wire mesh expecting a 10 mm cut, but the actual aperture is 11.5 mm, a good chunk of oversize will sneak through. Your client’s final product spec is now out, and the phone starts ringing. We see this most often on the Highveld, where quartzite and dolomite plants are pushing volumes, relying on accurate screening to meet their contracts.
Polyurethane panels are not immune. Under tension or when poorly installed, the aperture can stretch or deform, making matters worse. It is crucial to measure, not just trust what is printed or promised, especially when the screens are swapped on the fly after a power cut or a sticky day up in the Karoo.
How to check your apertures
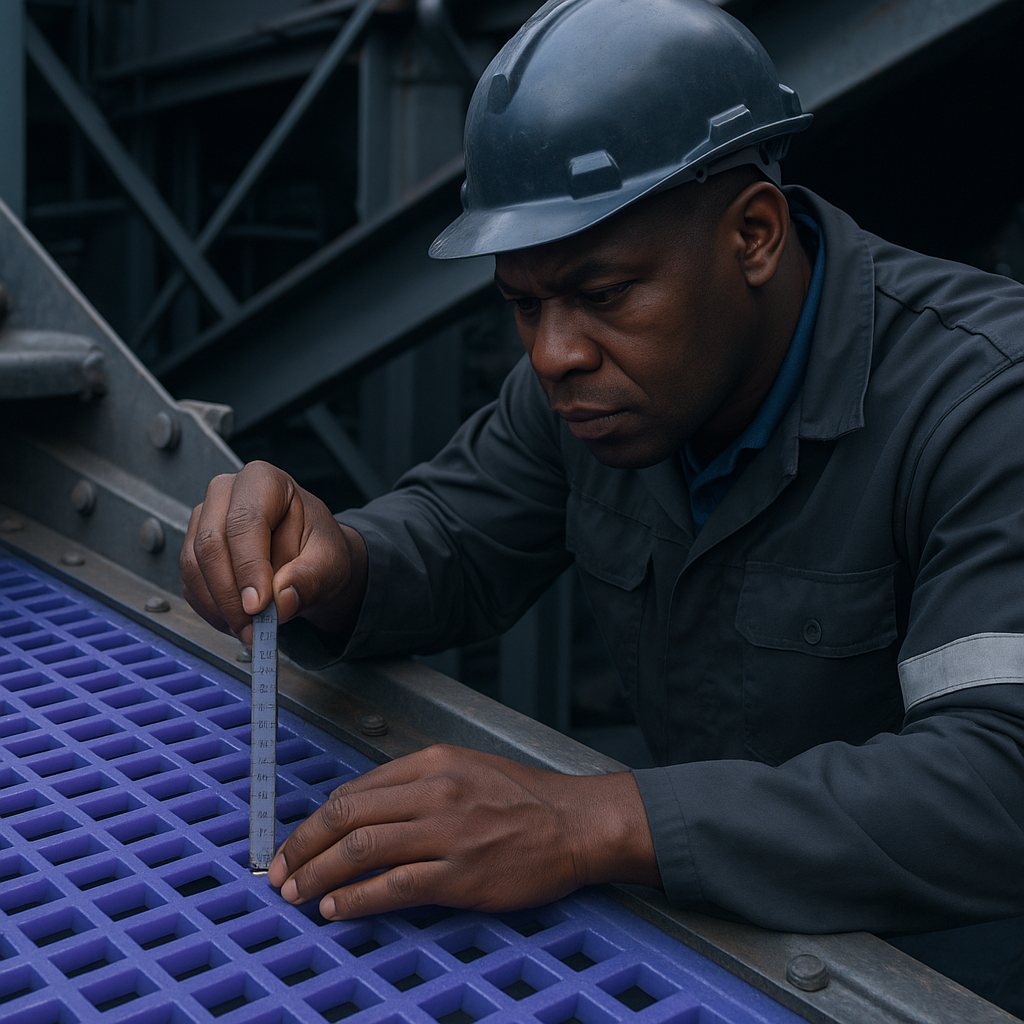
Never assume that a new mesh or panel is the size it claims. The best practice is to use a set of callipers or a wire gauge to measure several apertures across each panel, especially the centre and the edges. Check after the screen has been tensioned and bolted down, as tensioning can pull the mesh and alter the opening size.
For South African plants, where rapid temperature swings and dust can flex and clog screens, do these checks at least once per campaign, or whenever there is a change in screen batch or supplier. Record the readings and compare to what was ordered. If you spot a deviation of more than 0.5 mm, act immediately: this can mean the difference between an accepted and rejected load.
- Use a calibrated calliper for wire mesh
- Check polyurethane apertures after fitting
- Measure both before and after tensioning
- Document results for each deck and shift
Consequences of mismatched screens
Every rejected truck is not just lost revenue, it is also lasting damage to your reputation. We have seen contract crushers around Joburg and Durban lose long-term work because of a single run of out-of-spec sand or stone, traced back to oversize passing through a screen that lied about its aperture size. It is worse when the plant pushes the screens too far, hoping to stretch one more campaign, only for the opening to go out of range and let reject through.
Over time, poorly matched apertures also hammer the crushers downstream. Too much oversize going through to the cone or VSI means more recirculation, higher wear, and in many cases, a toggle plate snapping as the jaw tries to crush a rogue lump. The toggle is there as a fuse, but every time it breaks, you lose time and risk further damage.
Lessons from the field
We have seen the full range, from Lowveld sand plants running with DIY mesh stitched together, to big quarries in Gqeberha fitting panels that looked right until you measured them. The best performing clients are the ones who do not guess, but measure. They trust the numbers, not the label.
If you want to avoid rejected product and keep clients happy, make sure your foreman has the tools and the discipline to check every time. It is a small effort that saves tonnes of headache when the next batch leaves your weighbridge.
Related parts: Toggle Plate. You can also browse all parts and plant guides.
What our Crusher Wear Parts customers say
Verified Google reviews